Showing posts with label Bellow Valve. Show all posts

Monday, 15 June 2026

Bellows Seal Globe Valves in the Chemical and Specialty Chemical Industry

The global chemical industry handles thousands of process fluids — many of which are corrosive, toxic, carcinogenic, or environmentally hazardous. In such an environment, valve stem leakage is not merely an operational inconvenience; it is a serious safety and compliance risk. Bellows Seal Globe Valves have emerged as the valve of choice across chemical and specialty chemical plants precisely because they offer hermetic stem sealing that eliminates fugitive emissions at the source.

The Leakage Challenge in Chemical Processing

Conventional globe valves with graphite or PTFE packing are widely used across the process industry, but they carry an inherent limitation — packing degrades over time. In chemical plants handling aggressive media such as concentrated sulfuric acid, hydrochloric acid, caustic soda, and chlorinated solvents, even micro-leakage from the stem can lead to equipment corrosion, worker exposure, environmental contamination, and regulatory penalties. The economic and reputational cost of a fugitive emission incident in a specialty chemical plant can be severe, making zero-leakage stem sealing an operational necessity rather than a luxury.

Key Applications in Chemical Plants

Bellows seal globe valves are deployed extensively across multiple stages of chemical production. In reactor feed and discharge lines, they control the flow of reactive intermediates and catalysts where contamination or leakage could compromise product quality or trigger uncontrolled reactions. In distillation and separation columns, they manage the flow of volatile organic compounds (VOCs) and toxic process streams with precision. In heat exchanger circuits, where thermal cycling continuously stresses valve packing, bellows seal designs maintain their integrity far longer than conventional alternatives.

In specialty chemical manufacturing — covering products such as agrochemicals, dyes, adhesives, and electronic chemicals — process purity is as critical as safety. A bellows seal globe valve ensures that no external contamination enters the process through the stem area, and no process fluid escapes to the outside environment, meeting the dual requirement of containment and purity simultaneously.

Corrosion-Resistant Material Options

One of the key advantages of bellows seal globe valves in chemical service is the wide range of material options available. Body materials such as CF8M (SS 316), Alloy 20, Hastelloy C-276, and Inconel address the full spectrum of corrosive chemical media. Bellows fabricated from SS 316L offer excellent resistance to a wide range of acids and solvents, while exotic alloy bellows are available for highly aggressive media. This material flexibility makes bellows seal globe valves adaptable to virtually every chemical process fluid encountered in production.

Regulatory Compliance and Environmental Responsibility

Chemical plants worldwide are subject to increasingly stringent fugitive emission regulations. Standards such as ISO 15848-1, EPA Method 21, TA Luft (Germany), and the EU Industrial Emissions Directive mandate strict limits on VOC and toxic gas emissions from valve stems. Bellows seal globe valves, with their hermetic sealing design, consistently achieve the highest tightness classifications under these standards — making them the most reliable path to regulatory compliance in chemical processing environments.

Why Choosing the Right Manufacturer Matters

In chemical service, valve material selection, bellows weld quality, and corrosion resistance validation are critical factors that directly impact plant safety and operational continuity. Procurement teams must insist on full material traceability, third-party inspection, and corrosion testing documentation when sourcing bellows seal globe valves for aggressive chemical media. A valve that performs well in standard service may fail prematurely when exposed to concentrated acids or chlorinated compounds — making supplier expertise and quality certification non-negotiable.

Freture Techno Pvt. Ltd. is a leading Bellows Seal Globe Valve manufacturer in India, offering a comprehensive range of corrosion-resistant valves engineered specifically for chemical and specialty chemical applications. With expertise in exotic material construction, fugitive emission compliance, and rigorous quality testing, Freture Techno delivers bellows seal globe valves that chemical plants across India and global markets can depend on for safe, leak-free, and long-lasting performance.

Monday, 15 September 2025

Bellow Seal Valves in the Pharmaceutical Industry – Ensuring Purity and Safety

The pharmaceutical industry operates under strict quality and safety standards. Every component in the production process must ensure purity, precision, and compliance with regulatory norms. Valves, being critical to fluid handling, directly influence product quality and safety. Traditional valves, however, often struggle with leakage, contamination risks, and frequent maintenance. This is where Bellow Seal Valves play a vital role, providing leak-proof performance, contamination-free operations, and long-term reliability.

Challenges in the Pharmaceutical Industry

Pharmaceutical manufacturing requires stringent control over fluids, gases, and steam used in various processes. Even a minor leak can compromise product quality or violate compliance standards.

Common challenges include:

  • Risk of Contamination: Leaks or emissions can contaminate sensitive formulations.

  • Regulatory Pressure: Compliance with cGMP, FDA, and WHO norms demands zero leakage systems.

  • High Purity Requirements: Valves must not react with or alter the product.

  • Operational Downtime: Frequent valve failures can disrupt critical production schedules.

These challenges highlight the need for valves that combine precision, safety, and durability.

The Role of Bellow Seal Valves

A Bellow Seal Valve incorporates a metallic bellows that ensures a hermetic seal between the stem and the process medium. This design eliminates leakage, making it highly suitable for pharmaceutical environments where safety and purity are paramount.

Key Features:

  • Leak-Free Operation: Ensures zero stem leakage.

  • Sterile Design: Supports clean and contamination-free production.

  • Durability: Handles high-pressure and high-temperature conditions in sterile steam lines.

  • Regulatory Compliance: Designed to meet pharmaceutical validation standards.

Applications in Pharmaceutical Processes

Bellow Seal Valves are deployed in critical pharmaceutical applications such as:

  1. Pure Steam Distribution: Ensures sterile supply of steam without risk of leakage.

  2. Water for Injection (WFI) Systems: Prevents contamination in ultra-pure water pipelines.

  3. Chemical Dosing Lines: Provides safe handling of cleaning agents and solvents.

  4. Fermentation & Biotech Processes: Maintains sterile and controlled environments.

These applications demonstrate the valves’ role in protecting product quality and ensuring patient safety.

Benefits for the Pharmaceutical Industry

The adoption of Bellow Seal Globe Valves and Gate Valves brings several advantages to pharmaceutical operations:

  • Zero Contamination Risk: Leakage-free design ensures product purity.

  • Regulatory Compliance: Helps meet global pharmaceutical standards.

  • Operational Reliability: Reduces downtime in critical production stages.

  • Extended Service Life: Low maintenance requirements improve cost efficiency.

  • Worker Safety: Protects operators from exposure to harmful cleaning chemicals.

Why Bellow Seal Valves Are Preferred in Pharma

Unlike conventional valves, Bellow Seal Valves provide both precision flow control and contamination-free operations, making them indispensable for pharmaceutical manufacturing. Their ability to handle pure water, pure steam, and critical fluids without compromise ensures compliance and reliability.

With the growing global demand for high-quality medicines, pharmaceutical companies are investing in advanced technologies that guarantee safety and efficiency — and Bellow Seal Valves perfectly meet these expectations.

Conclusion

In an industry where safety, quality, and compliance are critical, Bellow Seal Valves provide unmatched reliability. By eliminating leakage, ensuring product purity, and meeting stringent international standards, these valves safeguard both production processes and end-user health.

For pharmaceutical companies committed to quality and safety, Bellow Seal Valves are an essential investment.

Freture Techno Pvt. Ltd., a leading manufacturer of Bellow Seal Valves in Mumbai, India, delivers advanced valve solutions trusted by pharmaceutical manufacturers worldwide.

Tuesday, 2 September 2025

Bellow Sealed Valve: Ensuring Zero Leakage and Maximum Safety

In industries where safety, reliability, and environmental compliance are non-negotiable, bellow sealed valves play a vital role. Unlike conventional valves that rely on stem packing for sealing, bellow sealed valves use a metallic bellows to provide a hermetic seal. This design eliminates the risk of external leakage, making them the preferred choice in sectors such as oil and gas, pharmaceuticals, chemicals, and power generation.

What Is a Bellow Sealed Valve?

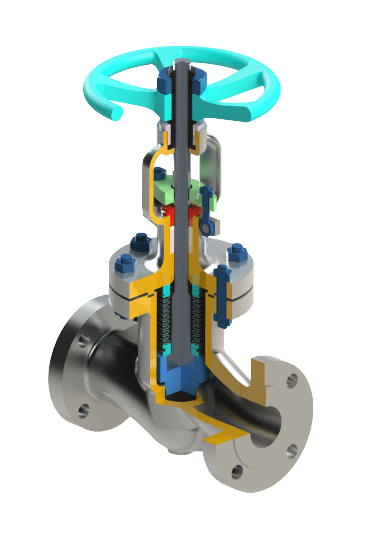
A bellow sealed valve incorporates a multi-ply metallic bellows welded to both the valve stem and bonnet. This creates a sealed barrier between the fluid and the atmosphere. The bellows expand and contract with stem movement, ensuring precise operation without compromising the seal. As a result, these valves offer zero-emission and long-lasting sealing performance, even in harsh operating environments.

Key Features and Benefits

  • Zero Leakage: Eliminates fugitive emissions, ensuring compliance with strict environmental standards.

  • Long Service Life: Bellows are designed for thousands of cycles without failure.

  • Enhanced Safety: Prevents hazardous leaks in chemical and toxic service applications.

  • Low Maintenance: Fewer sealing components mean reduced wear and minimal servicing.

  • High Performance: Capable of withstanding high pressures, extreme temperatures, and corrosive media.

Challenges with Conventional Valves

Traditional valves that rely on stem packing often face:

  • Leakages over time due to packing wear and tear.

  • Increased risk of fugitive emissions, leading to regulatory issues.

  • Frequent maintenance, causing downtime and operational inefficiency.

  • Safety concerns when handling toxic, flammable, or radioactive media.

This is why industries are shifting toward reliable bellow sealed valve manufacturers who can guarantee leak-free operation.

Applications of Bellow Sealed Valves

Bellow sealed valves are indispensable in industries where absolute sealing is required:

  • Pharmaceuticals: In purified water systems and chemical handling processes.

  • Oil & Gas: For preventing hydrocarbon leaks in pipelines and refineries.

  • Chemical Industry: Handling corrosive, hazardous, or high-purity chemicals.

  • Power Plants: Managing steam and condensate with zero leakage.

  • Nuclear Facilities: Ensuring complete containment of radioactive fluids.

Industry Trends and Advancements

The demand for safer and more efficient valves has led to several innovations:

  • Bizmon bellows technology that enhances flexibility and durability.

  • Zero-emission globe and gate valve designs meeting strict international standards.

  • Use of exotic alloys like Hastelloy and Inconel for high-corrosion resistance.

  • Integration with automation systems for remote monitoring and control.

These advancements make bellow sealed valves not just safer but also smarter, aligning with modern industrial requirements.

Why Choose Reliable Bellow Sealed Valve Manufacturers?

Working with the right manufacturer ensures:

  • Proven compliance with global standards such as ISO, PED, and API.

  • Advanced design engineering for long cycle life and superior performance.

  • Customization to meet unique industrial demands.

  • Guaranteed support with material certifications and test reports.

The bellow sealed valve is more than just a flow control device—it is a safeguard against leaks, emissions, and safety risks. With zero leakage, long service life, and unmatched reliability, it has become essential for industries handling critical processes. As environmental regulations tighten and safety standards rise, partnering with a Zero leakage Bellow Sealed Valve manufacturer ensures operational efficiency, compliance, and peace of mind.

Tuesday, 25 February 2025

Bellow Sealed Globe Valve: Enhancing Industrial Efficiency and Reliability

In the world of industrial fluid control, the Bellow Sealed Globe valve has emerged as a critical component for systems that demand precision, reliability, and leak-free operation. These valves are designed to offer excellent sealing performance in high-pressure and high-temperature environments, making them indispensable in sectors ranging from chemical processing to power generation.

What is a Bellow Sealed Globe Valve?

The valve is a specialized type of valve that incorporates a flexible bellow as its sealing element. Unlike conventional valves that rely solely on traditional packing materials, the bellow provides a dynamic seal that effectively prevents leakage. The globe valve’s inherent design allows for precise flow regulation, while the bellow element ensures that even under extreme conditions, the seal remains intact. This unique combination of design features enhances the overall performance of the valve, making it suitable for critical applications where safety and efficiency are paramount.

Bellow Sealed Globe Valve by Freture Techno


Key Features and Benefits

Enhanced Sealing Capability:
The primary advantage of a these Globe valve is its superior sealing performance. The integrated bellow adapts to changes in pressure and temperature, maintaining a tight seal that minimizes the risk of leaks. This is particularly important in processes involving hazardous or corrosive fluids, where any leakage could lead to severe safety and environmental consequences.

Precise Flow Control:
Globe valves are renowned for their ability to regulate flow with high accuracy. The bellow sealed design further refines this control by reducing the effects of thermal expansion and vibration. This means operators can adjust flow rates with confidence, ensuring that systems run smoothly and efficiently.

Durability and Longevity:
Industrial environments often subject valves to harsh conditions, including extreme temperatures and corrosive substances. The Bellow Valve is engineered with robust materials and construction techniques that resist wear and tear. This durability translates into a longer service life, reducing the frequency of maintenance and replacement, and ultimately lowering overall operational costs.

Minimal Maintenance Requirements:
One of the key selling points of Bellow Sealed Globe valves is their reduced need for routine maintenance. The bellow’s ability to maintain a consistent seal minimizes the wear on other valve components, which in turn reduces the likelihood of unexpected breakdowns. For industries where uptime is critical, this means fewer disruptions and increased productivity.

Adaptability Across Industries:
From petrochemical plants and water treatment facilities to power generation stations, the versatility of the bellow sealed globe valve makes it a preferred choice in a wide range of applications. Its design is adaptable enough to handle various fluid types and process conditions, making it a universal solution for many industrial challenges.

Applications in Modern Industry

The Globe Valves are integral to systems where precision and reliability cannot be compromised. In the chemical processing industry, these valves help control the flow of reactive substances, ensuring that processes remain safe and efficient. In power plants, they regulate steam and water flow, playing a vital role in maintaining system stability and performance. Additionally, in water treatment and waste management systems, the valves provide the necessary control to prevent contamination and ensure compliance with strict regulatory standards.

Innovations and Future Trends

The evolution of industrial automation and digital monitoring has paved the way for smarter, more integrated valve systems. Modern Bellow Sealed Globe valves are now often equipped with sensors that provide real-time data on pressure, temperature, and flow rates. This integration with the Industrial Internet of Things (IIoT) allows for predictive maintenance and improved process control. By monitoring performance continuously, operators can anticipate issues before they become critical, thereby enhancing operational efficiency and safety.

Conclusion

The Globe valve is a prime example of engineering innovation meeting practical industrial needs. Its superior sealing capability, precise flow control, durability, and low maintenance requirements make it a cornerstone in modern industrial processes. As industries continue to demand higher efficiency and safety standards, the role of advanced valve technologies like the Bellow Sealed Globe valve will undoubtedly grow. For engineers and facility managers looking to optimize their systems, investing in these valves offers a pathway to improved performance and long-term operational cost savings.

With continuous advancements in materials and sensor technology, the future of These Globe valves is promising. They will continue to play a vital role in ensuring that industries operate at peak efficiency, providing the secure, reliable, and precise control that modern processes require. Whether you are involved in chemical processing, power generation, or water treatment, understanding and utilizing the benefits of these Globe Valves can be a game changer for your operations.

Wednesday, 25 October 2023

Environmental Impact of Valve Leakage: A Silent Threat to Our Ecosystem

Industrial valves are essential components in various sectors, facilitating the control of fluids and gases. However, the unnoticed culprits, valve leaks, can cause severe environmental damage. In this article, we will explore the environmental impact of valve leakage, emphasizing the importance of addressing this silent threat.

The Hidden Consequences

Valve leakage may appear as a minor issue in isolation, but its collective impact is staggering. These leaks release harmful substances into the environment, affecting both terrestrial and aquatic ecosystems. The consequences are far-reaching and often underestimated.

Soil Contamination

Leaking valves often release corrosive chemicals, hydrocarbons, or toxic substances, which can seep into the soil. The contaminated soil loses its fertility, rendering it unsuitable for agriculture. Over time, this can lead to the degradation of large tracts of arable land.

Water Pollution

Valve leaks can contaminate nearby water bodies. Chemicals and pollutants from these leaks find their way into rivers, lakes, and oceans. Aquatic life can be severely impacted, with devastating effects on fish populations and the delicate balance of aquatic ecosystems.

Air Quality

In some cases, valve leaks release volatile organic compounds (VOCs) into the air. These can react with other pollutants to form ground-level ozone, a major component of smog. Poor air quality affects human health, and it contributes to global warming.

Biodiversity Loss

The destruction of ecosystems due to valve leakage disrupts the habitats of countless species. Plants and animals that rely on these ecosystems face the risk of extinction. Biodiversity loss has long-term consequences for the planet's ecological balance.

Preventive Measures

Preventing valve leakage is crucial in reducing its environmental impact. Regular maintenance, inspection, and the use of high-quality, zero-leakage valves can significantly minimize these issues. Additionally, adopting eco-friendly practices and materials in valve construction can further reduce environmental harm.

Zero-Leakage Valves: A Green Solution

Bellow Sealed Globe Valve

Zero-leakage valves, as the name suggests, are designed to prevent any form of leakage. These valves are crafted from materials that are highly resistant to corrosion, wear, and tear. By adopting zero-leakage valves, industries can substantially reduce their environmental footprint. This solution offers several benefits:

Reduced Environmental Liability: Zero-leakage valves help industries comply with environmental regulations, preventing costly fines and remediation expenses.

Resource Conservation: Preventing leaks conserves valuable resources and reduces the need for energy-intensive pollution control measures.

Improved Corporate Image: Embracing green technology enhances a company's reputation, demonstrating a commitment to environmental responsibility.

Valve leakage is a significant environmental concern with far-reaching consequences. It affects not only natural ecosystems but also human health and industry reputation. By adopting zero-leakage valves and implementing eco-friendly practices, industries can mitigate these environmental impacts and play their part in safeguarding the planet for future generations. It's time to recognize the silent threat of valve leakage and take proactive steps to protect our environment.

Bellows Seal Globe Valves in the Chemical and Specialty Chemical Industry

The global chemical industry handles thousands of process fluids — many of which are corrosive, toxic, carcinogenic, or environmentally haza...